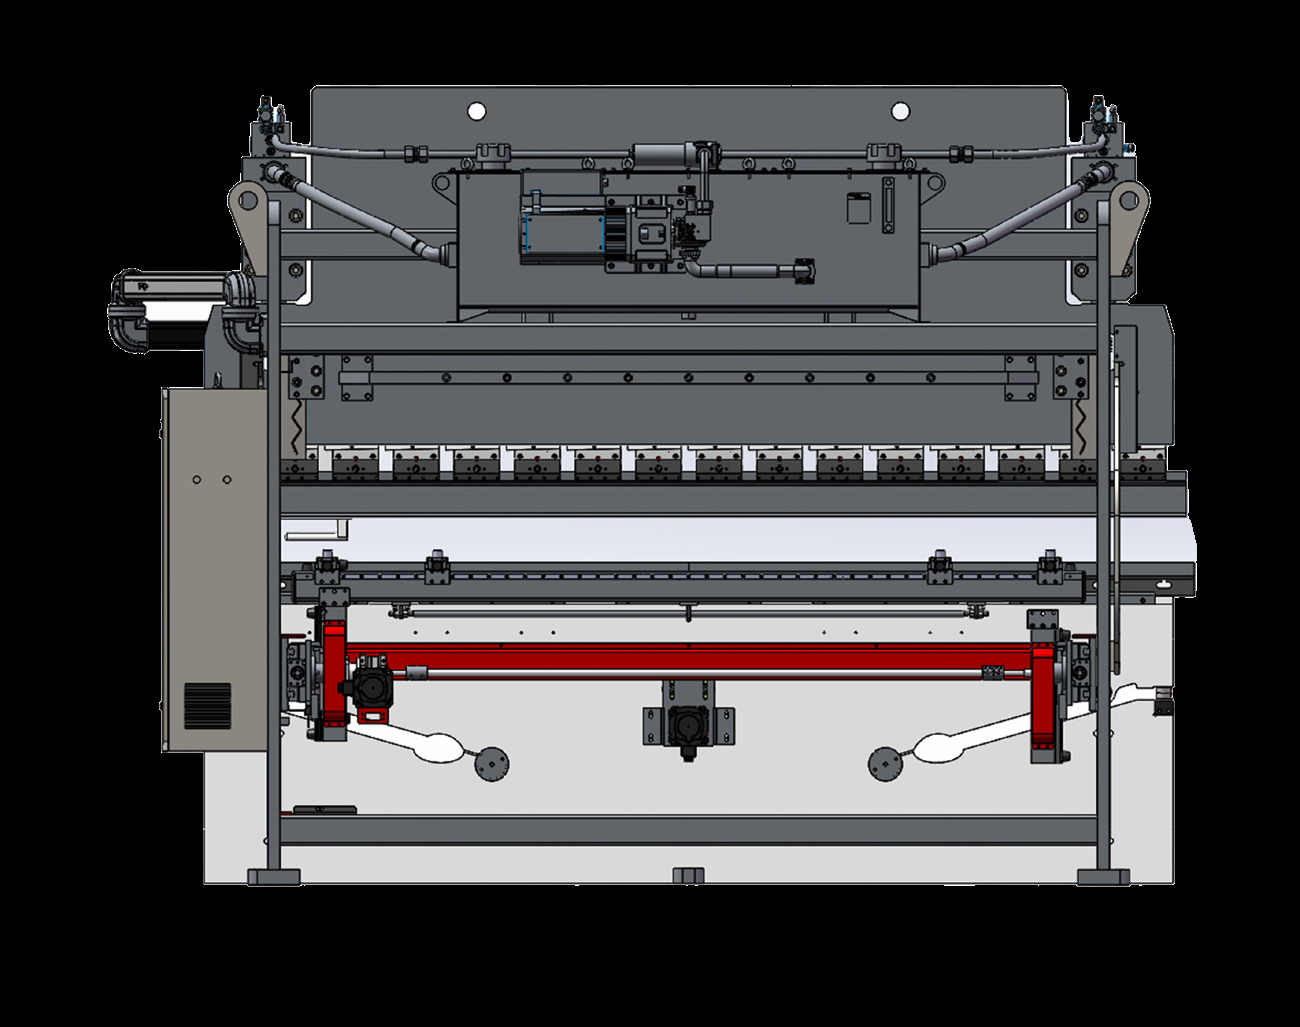
A press brake affects angle quality, throughput, setup time, operator workload and future capacity. A useful specification therefore describes the complete bending process rather than selecting force and working length in isolation.
What material and thickness will you bend?
Material strength and thickness determine required force. Mild steel, stainless steel and aluminum do not require the same tonnage for the same bend. Grain direction, tensile variation and surface requirements also affect tooling and process selection.
What is the maximum loaded bend length?
Working length should cover the longest actual bend while leaving practical room for loading and tooling segmentation. Long beds can reduce flexibility and increase cost when most work is short; undersizing creates an immediate production constraint.
Which flanges and formed shapes must clear the machine?
Small return flanges, deep boxes and staged profiles influence throat depth, open height, stroke and backgauge axes. Review the complete part sequence, not only the first bend.
Complex parts may benefit from R-axis height movement, independent Z fingers, six-axis gauging, graphical simulation and front support systems.
How often will jobs repeat?
High-mix work values quick programming, tool libraries and flexible gauging. Repetitive production values cycle speed, automatic correction, ergonomic handling and offline preparation. The same part can justify different machines at different annual volumes.
Which drive architecture fits the application?
Best suited to compact precision work where fast response, low idle energy and oil-free operation matter.
Covers broader force and length ranges while reducing unnecessary pump operation, heat and noise.
Used when part length, force, daylight or handling exceeds a standard single-machine envelope.
Will the machine use new or existing tooling?
Tool style, load rating, punch height and clamping interface affect daylight and usable stroke. Compatible pre-owned tools may be retained with engineered adapters and safety clamps after inspection.
What must happen before production release?
Confirm floor loading, electrical supply, unloading access, operator training, safeguarding and inspection requirements before delivery. BENDRYX coordinates North American application review, commissioning planning, parts and service support.
Selection checklist
Send the information that changes the machine.
- Material grades and thickness range
- Longest bend and highest-force bend
- Part drawings and bend sequence
- Annual volume and target cycle
- Existing tooling details
- Floor, power and loading constraints